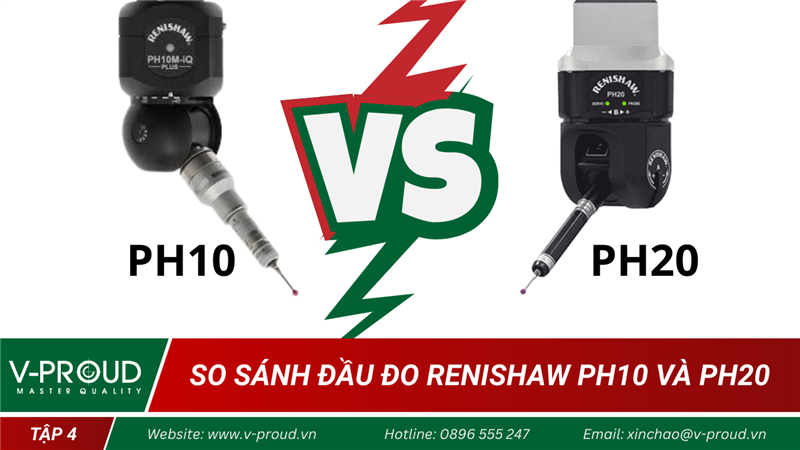
Using older 3D CMM measuring machines is a temporary solution to save costs and address measurement and quality control issues in small and medium-sized enterprises with limited capital. Therefore, Renishaw has researched and launched measuring head systems that significantly upgrade and improve measurement capabilities using only PH10 and PH20 measuring heads.
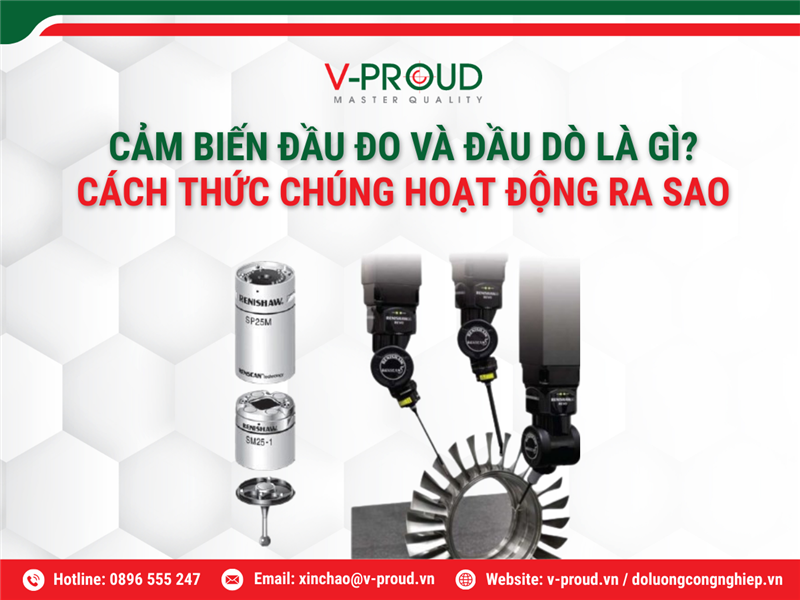
Renishaw probes and sensors are the core foundation in coordinate measurement (CMM) and machine tool measurement (CNC) technology. These devices act as the first link directly connecting to the workpiece, allowing the machine to collect X, Y, and Z coordinate data to calculate the dimensions, shape, and position of geometric features.
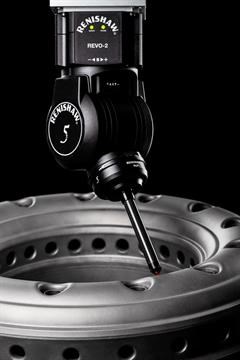
The RUP1 (Ultrasonic Probe) module is one of the most unique accessories of the Renishaw REVO 5-axis system. It allows the CMM to perform material thickness measurements using ultrasonic waves. With the Renishaw REVO 5-axis RUP1, you can measure the thickness of walls without needing to approach from both sides. This is an extremely useful solution for the aerospace industry, where the Renishaw REVO 5-axis is used to inspect hollow turbine blades.
Their ability to measure precisely, quickly and without contact, plus the option to integrate the results of these measurements into the production process directly, leads to increased productivity.
To ensure consistent quality is achieved when manufacturing many different devices or components, the results of the production process need to be checked regularly by taking measurements. These checks are performed in various ways: either outside of the ongoing process, by regularly removing individual devices and checking them using appropriate mechanical or optical measuring instruments; or via measuring stations integrated into the process, which are equipped with mechanical sampling systems or other non-destructive measuring instruments. Optical measurement sensors are ideal for integration into the manufacturing process.
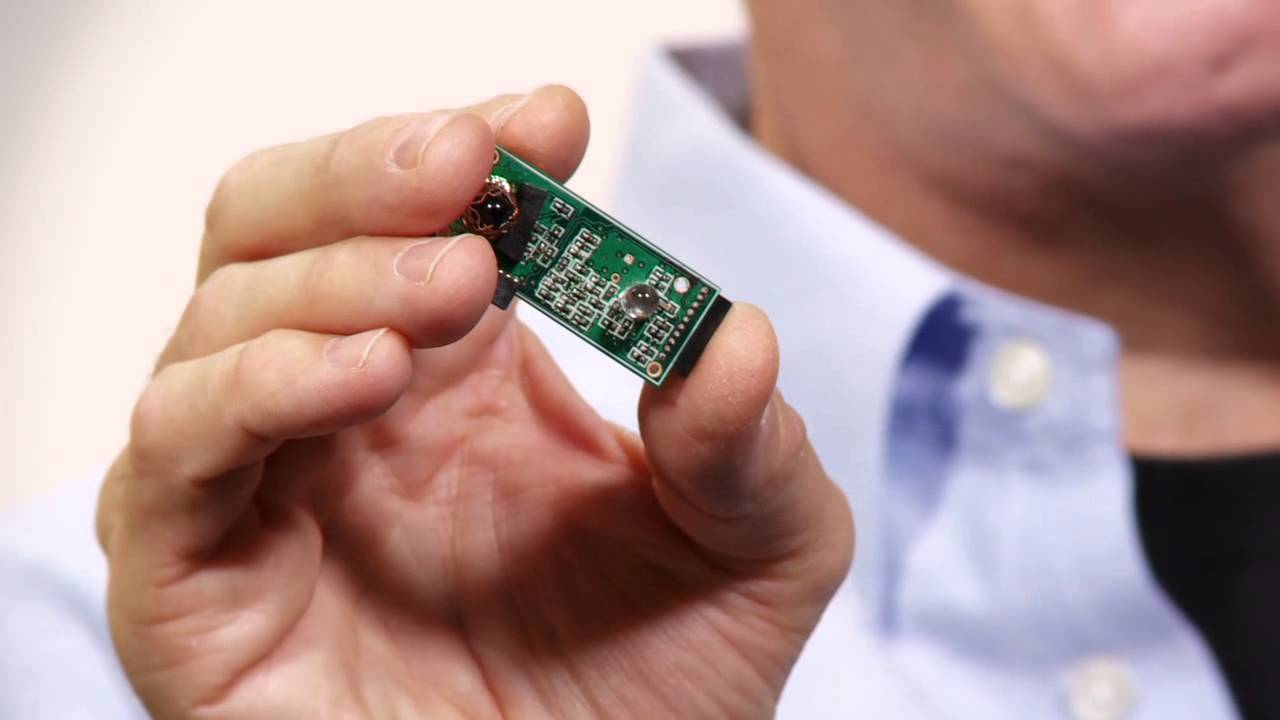
Their ability to measure precisely, quickly and without contact, plus the option to integrate the results of these measurements into the production process directly, leads to increased productivity. This results in faster production processes at a consistently high quality, without the need to make mechanical contact with the object or damage it in any way. Optical sensors provide extremely accurate results even when measuring very small objects.
Various technologies are used to create precise optical measurement sensors with the most popular being:
Laser Triangulation Principle
Laser triangulation is a single- or multi-dimensional distance measurement resulting from an angular calculation. The sensor projects a laser light onto the measuring object. The beam reflected there is then mapped, via optics, to a particular place on a position-sensitive receiver element, depending on the distances involved. The distance to the measuring object is determined by triangulating the light source, the measuring point on the object, and the image of the light on the receiver element. Sensors are available with light spots of different sizes. It is better to use small light spot geometries for very small objects, whereas a sensor with a larger light spot is recommended for rough surfaces.
The same principle of operation also applies to sensors which use not a light spot, but a laser line, combined with a CMOS matrix receiver. In this case, a profile can be detected and evaluated directly, without having to move the object.
Chromatic-Confocal and Interferometric Measurement Principle
Chromatic-confocal measurement sensors use white light sources, whose light spectrum is directed to the measurement head via optical fibers. The OC Sharp displacement measurement sensor from SICK allows the user to choose from two different measuring methods.
The lens system integrated in the measurement head has been designed such that the individual wavelengths are all assigned to a different distance. OC Sharp makes use of chromatic aberration, which is usually an unwanted effect. Each wavelength is focused at a different distance, reflected by the surface, and the reflected wavelength is then evaluated in a spectrometer. The wavelength determined is assigned to a distance value in turn.
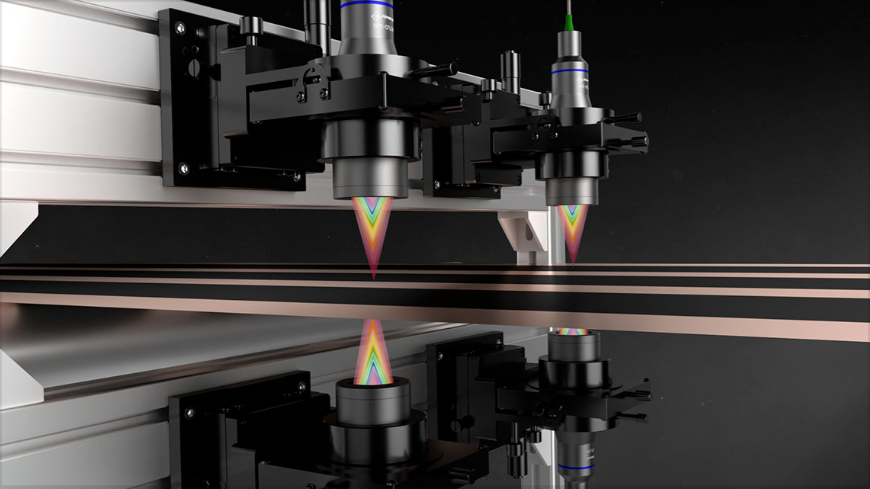
As with many sensors which operate according to the laser triangulation principle, several reflected wavelengths can be evaluated in this case too, thus enabling a relative material thickness to be determined for single- or even multi-layered transparent objects.
Interferometric Measuring Method
The interferometric measuring method uses the physical effect of interference on thin layers. We are familiar with this effect from puddles that shimmer with color, caused by a thin film of oil, or from soap bubbles, for example. Different wavelengths of the light are either weakened or strengthened by specific material thicknesses. A quick Fourier transformation is then used to evaluate the spectrum of the detected layers. Unlike with the chromatic-confocal measuring method, here it is not possible to evaluate an absolute distance, but just the thicknesses present in a system of layers.
Significant advantages over the laser triangulation principle are exhibited including:
Challenges
There are many reasons to use optical measuring instruments:
When changing over to optical measuring instruments, a challenge which sometimes has to be met is how to achieve results that are comparable with those previously obtained by mechanical means.
Due to the different ways in which optical and mechanical measuring instruments work, the following must be taken into consideration:
The process of changing over from a mechanical to an optical measuring instrument can be quite costly and laborious; however, this must be balanced against the long-term benefits such as cost savings, increased throughput, no mechanical impact on the measuring object, and improved quality in every process step.
Read Quality Mastery magazine to get more information about quality management: https://qualitymastery.v-proud.vn/
If you are looking for quality management solutions, visit the following websites: v-proud.vn/product and doluongcongnghiep.vn.
Source: sick

(84) 896 555 247
 Tiếng Việt
 English